In injection molding, gate design determines where molten plastic enters the cavity and how effectively the part can be filled and packed. It also affects the mark left after molding and the work required to remove the gate.
The right choice depends on the finished part. A gate that fills the cavity successfully may still leave an unacceptable mark on a visible surface, interfere with a mating edge, or make automatic production difficult.
Before tooling begins, review gate type, location, dimensions, and removal method together. This guide explains how to compare those choices and what to verify during mold trials.
What Is a Gate in Injection Molding?
A gate is the opening through which molten plastic enters the mold cavity from the melt delivery system.
Gate design includes more than selecting this entry point. It also defines the passage geometry, the number of entry points, and how the finished part separates from the feed system.
For a cold-runner mold, the gate must allow adequate filling and packing before it freezes. For a hot-runner system, thermal control and, where applicable, valve timing also influence how material enters the cavity.
In both cases, the gate must meet the requirements of the molded part and the intended production process.
Injection Molding Gate Types: A Practical Comparison
Use the following comparison to shortlist gate options. Final selection requires the actual part geometry, resin grade, and mold layout.
| Gate type | When to consider it | Main limitation |
|---|---|---|
| Edge gate | A parting-line edge is available and a straightforward cold-runner arrangement is suitable | Trimming access and the remaining edge mark must be acceptable |
| Tab gate | A removable tab can accommodate the entry area outside the finished part profile | Requires space for the tab and controlled removal |
| Fan gate | A broader entry is useful for evaluating flow into a wide, relatively thin part | Creates a wider attachment that generally requires trimming |
| Pinpoint gate | A small entry and automatic runner separation suit a three-plate mold layout | Restricted flow passage and additional mold-opening requirements |
| Tunnel or submarine gate | Automatic gate separation is desirable and the material and geometry allow it | Gate breakage, runner release, and damage during ejection must be checked |
| Direct sprue gate | Direct feeding is suitable for a relatively large or thick part | A substantial gate mark and removal operation may be required |
| Thermal hot-tip gate | Direct hot-runner feeding suits the material, geometry, and production plan | Gate vestige, blush, and temperature control require attention |
| Valve gate | Controlled gate opening and closing justify a more complex hot-runner system | Higher tooling complexity, maintenance needs, and control requirements |
Gate names can vary between suppliers. For example, “pin gate” may describe different arrangements. Ask for a section view showing the entry passage and separation method rather than approving a name alone.
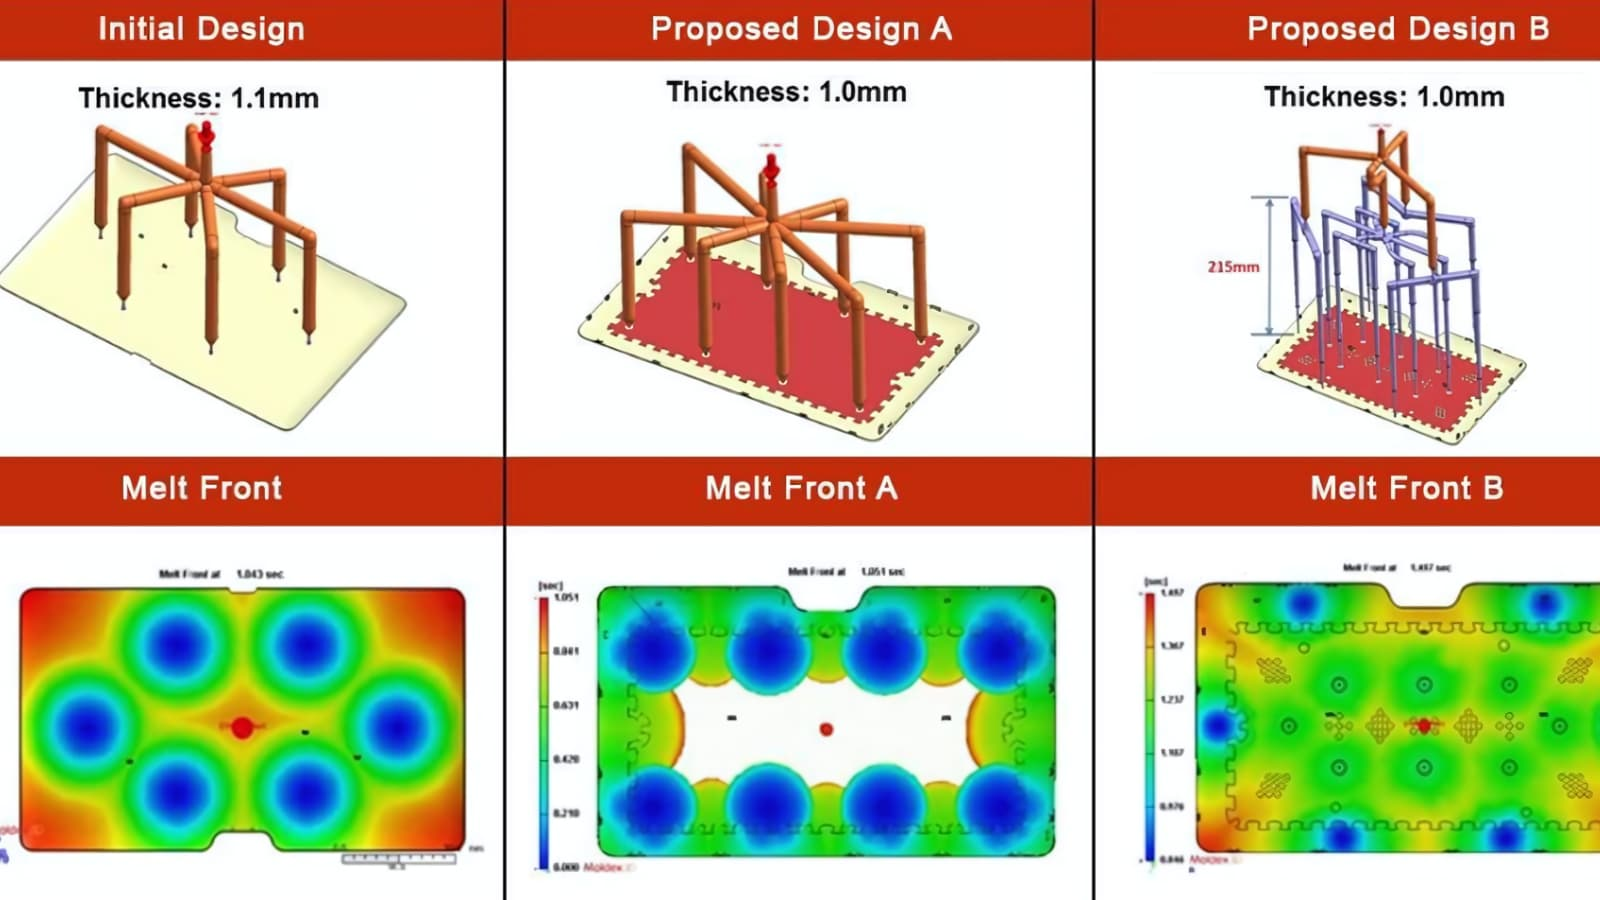
Thermal hot-tip gates and valve gates should also be distinguished. A thermal gate relies on temperature and local solidification behavior, while a valve gate uses a moving pin to control the opening.
For the broader tooling decision, see our cold runner vs. hot runner comparison.
How to Choose the Gate Location
Start With Appearance and Assembly Restrictions
Mark the areas where a gate or residual mark is unacceptable. These may include visible faces, sealing tracks, mating edges, and loaded features.
A less visible location is often preferable, but visibility is only one requirement. A hidden gate mark on a cover joint can still prevent the housing from closing correctly.
The drawing should identify both the permitted gate area and the acceptable condition after trimming.
Review Wall Thickness and Flow Paths
Where practical, position the gate so material can feed a thicker region without first passing through a thin restriction that may freeze early.
However, the shortest flow path is not always the best arrangement. Openings, ribs, wall transitions, and material orientation can change how the cavity fills.
A central gate may help balance some geometries, while long, narrow parts may need a different approach. For reinforced materials, review how the proposed flow direction could affect fiber orientation and dimensional behavior.
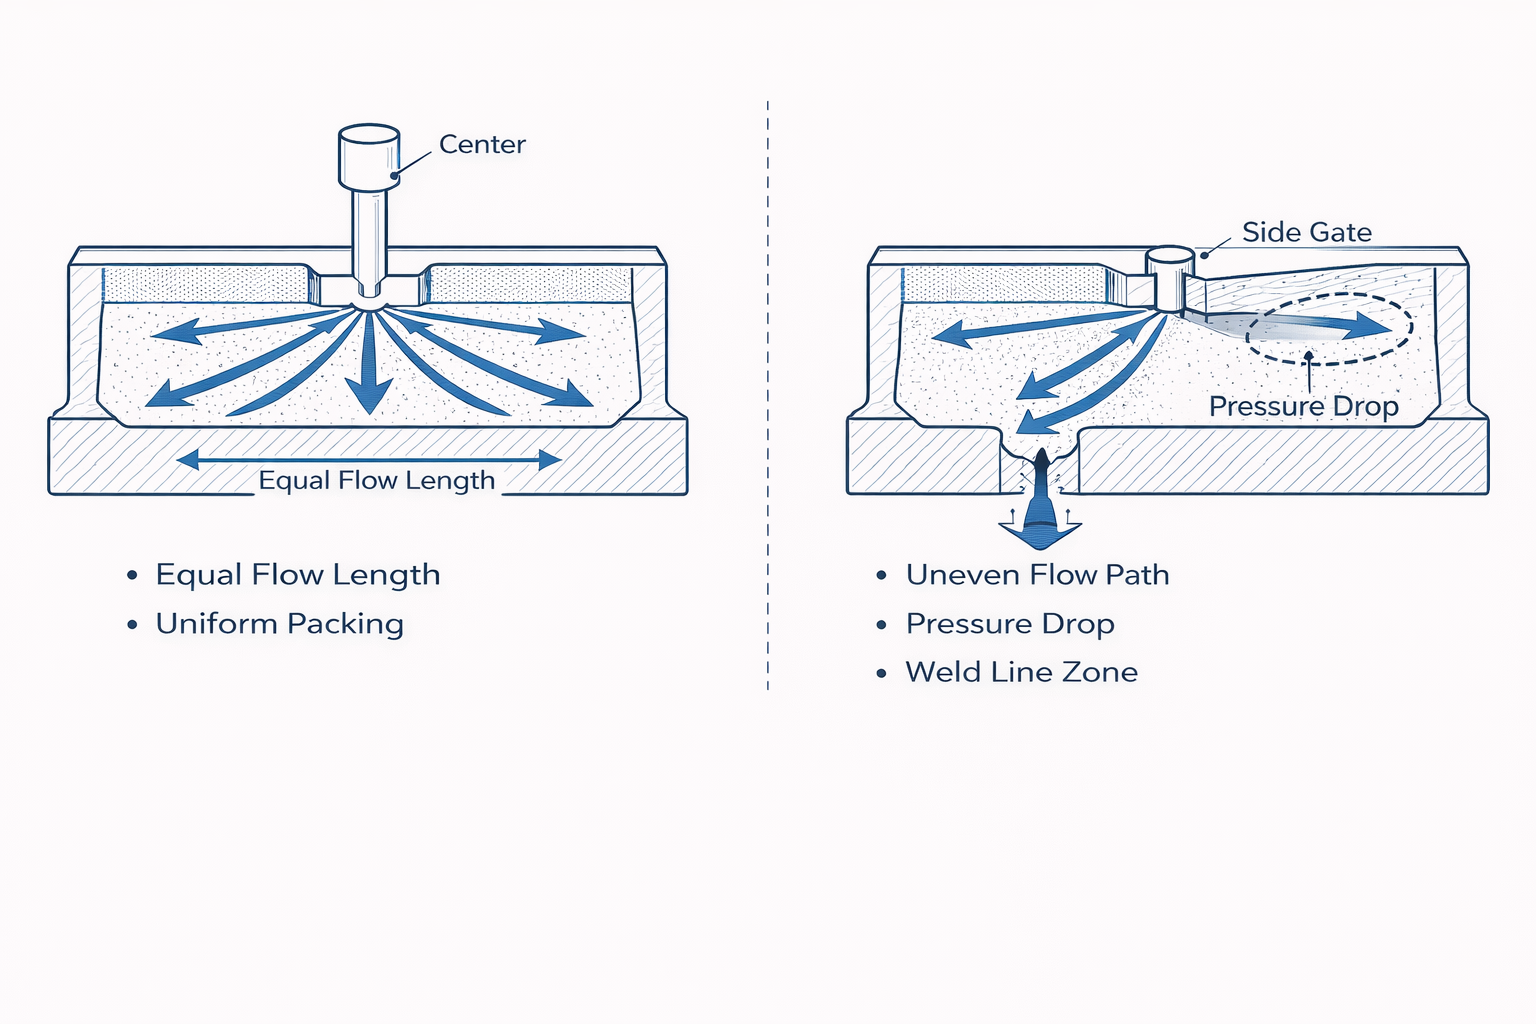
Autodesk’s injection-location design guidance explains several of these placement considerations.
Check Weld Lines and Venting Together
When melt flows around an opening, separate flow fronts may meet on the opposite side. Review where this meeting region falls relative to clips, screw attachments, sealing features, and visible surfaces.
At the same time, identify where air will escape from the areas that fill last.
Adding another gate may shorten the filling distance, but it also changes the flow-front pattern and can introduce additional weld lines. Evaluate the complete layout before treating another gate as the solution.
Consider Ribs and Bosses in Context
A rib or boss near the gate is not automatically a design error. Its effect depends on the local geometry, wall thickness, entry direction, and packing conditions.
Review whether the arrangement produces an abrupt flow change, a difficult-to-vent region, or excessive local material thickness. Avoid applying a blanket rule that every gate must be a fixed distance from every rib or boss.
For related structural considerations, see our plastic enclosure design guide.
How to Determine Gate Size and Packing Requirements
There is no universal gate diameter or gate-to-wall-thickness ratio that works for every part.
The starting dimensions should account for:
- The exact resin grade and any reinforcement.
- Part volume and local wall thickness.
- Gate cross-section and land length.
- Expected filling rate and pressure loss.
- Packing requirements.
- Permitted gate mark and removal method.
The gate land is the short restricted passage at the cavity entrance. Two gates with the same opening size can behave differently if their passage geometry differs.
An overly restrictive gate may increase shear and pressure loss or freeze before sufficient packing has occurred. Enlarging it can improve feeding, but may also create a larger trimming area or extend the solidification time of a cold gate.

Gate sizing therefore needs to balance molding performance with finished-part requirements.
For cold gates, a gate-seal study can help evaluate packing time. Under controlled conditions, the team increases holding time and measures part weight to identify when further holding no longer adds material. Interpret the result alongside filling consistency, cushioning, and other process conditions.
For valve gates, review the packing sequence together with valve-closing timing rather than applying a cold-gate freeze-off test unchanged.
Example: Selecting a Gate for a Plastic Enclosure
This is an illustrative design review, not a customer case or a tested production result.
Consider a rectangular PC/ABS enclosure with a textured front face, a display opening, internal screw bosses, and a cover joint around its perimeter.
The front surface must remain visually consistent, and the cover joint must close without interference.
Three candidate arrangements could be reviewed:
| Candidate | Reason to evaluate it | Question to resolve |
|---|---|---|
| Edge or tab gate on a less visible edge | Provides an accessible trimming location | Will the trimmed area interfere with the cover joint? |
| Tunnel gate into a suitable hidden area | May support automatic separation | Can the gate and runner release without damaging the housing? |
| Direct hot-runner entry at an approved location | Offers another way to arrange the filling path | Are the gate mark, system cost, and maintenance requirements acceptable? |
Compare these options using the actual CAD model. Show the proposed gate entry, removal access, flow around the display opening, and relationship to the screw features.
Where flow simulation is used, compare the alternatives with consistent material and process assumptions. Then verify the selected arrangement during trials.
The approval should address both molding behavior and the assembled product. Hiding the gate is not enough if the finished housing fails its fit or appearance requirements.
Gate Removal, Automation, and Maintenance
Decide how the gate will be removed before approving its location.
For manually trimmed gates, confirm tool access and the permitted remaining mark. An awkward trimming operation may produce whitening, uneven edges, or damage to an adjacent surface.
For automatic separation, verify that the gate breaks consistently and that the runner clears the mold. Automatic degating depends on material behavior and release geometry; it should not be assumed from the gate name alone.
Hot-runner systems remove the conventional cold runner at the part, but the gate area can still require appearance inspection.
For abrasive materials or demanding production volumes, also review access for maintenance. Replaceable gate inserts may be useful where wear or future adjustment is expected.
What to Check During Mold Trials
A successful first sample does not establish a stable production process. Gate validation should include repeated cycles under the intended operating conditions.
| Check | What it helps verify |
|---|---|
| Controlled short-shot study | Flow progression, hesitant regions, and filling balance |
| Packing study | Whether material continues to feed the part as intended |
| Gate-area inspection | Vestige, blush, whitening, and trimming damage |
| Dimensional and assembly checks | Fit after the specified conditioning period |
| Repeated automatic cycles | Consistent separation and runner removal |
| Multi-cavity comparison | Differences in filling, part weight, dimensions, and appearance |
For multi-cavity molds, a geometrically balanced runner layout does not guarantee identical behavior in every cavity. Review temperature, gate geometry, flow conditions, and cooling differences.
For sequential valve gating, include opening and closing timing in the trial record.
Our mold trials and mass-production guide explains why sampling conditions should represent the intended production process.
Gate Design Approval Checklist
Before releasing the mold design, confirm:
- The gate type and position are shown on the approved drawing.
- The resin grade and part revision are identified.
- Proposed gate dimensions and adjustment options are documented.
- Cosmetic, sealing, and assembly restrictions are marked.
- Gate removal and the acceptable residual mark are defined.
- Filling, weld-line, and venting risks have been reviewed.
- Trial checks and acceptance criteria are agreed.
An approval that says only “gate position accepted” leaves important details unresolved.
Frequently Asked Questions
What Is the Best Gate Type for Injection Molding?
There is no single best gate type. Compare the options against part geometry, resin, mold construction, appearance requirements, and the production plan.
Should a Gate Be Located in a Thick or Thin Section?
Where practical, feeding a thicker region can help maintain an effective packing path. However, the complete geometry, flow direction, and appearance restrictions must also be considered.
Can a Gate Leave No Visible Mark?
Do not assume that a gate will be invisible. Gate design and location can reduce its impact, but the acceptable appearance should be defined and checked on samples.
Can Changing the Gate Solve Sink Marks?
It may help when restricted feeding or early gate freeze contributes to the problem. It will not automatically correct excessive local wall thickness or unsuitable process conditions. Review the cause before modifying the mold.
Can Gate Design Be Changed After the Mold Is Built?
Some changes are possible, particularly when adjustment has been considered in the tooling design. However, moving an entry point or changing the gate system may require substantial rework. Review the proposal before cutting steel.
Discuss Gate Requirements Before Tooling
A useful gate proposal explains how the part will fill, how the gate will separate, and what the finished surface will look like.
If you are preparing a plastic enclosure or molded component for production, send CINDY MOULD the 3D model, resin specification, expected quantity, and marked cosmetic and assembly requirements.
Explore our enclosure manufacturing services or send your project requirements for review.